10 Tips for Choosing an Automotive Spot Welder?

Choosing an automotive spot welder is not simply a matter of comparing amperage and price. In a busy repair bay, the wrong machine can create weak joints, scorched panels, or uneven weld marks. A practical choice starts with vehicle materials, panel thickness, power supply, and daily workload. Technicians should also inspect electrode reach, clamping force, cooling performance, and control accuracy. Small details matter.

This guide presents ten practical tips for evaluating a spot welder before purchase. The recommendations reflect common workshop requirements, manufacturer specifications, and established vehicle repair practices. A dependable machine should support consistent weld penetration without damaging galvanized steel or nearby components. It should also provide clear settings, stable current delivery, and accessible maintenance points. Easy controls help, but they cannot replace proper training. Experience helps, though it can sometimes create bias.

Look beyond the sales brochure. Ask whether the equipment matches the vehicle manufacturer’s repair procedures and local electrical safety requirements. Check duty cycle ratings under realistic shop conditions, not only laboratory claims. Review warranty coverage, spare electrode availability, software support, and service response times. These factors can affect downtime more than a small difference in purchase price. A useful test includes repeated welds on similar metal panels, followed by visual and destructive quality checks where appropriate. That extra step may feel slow. It often reveals problems early. The ten tips ahead will help buyers compare performance, safety, usability, and long-term value with greater confidence.
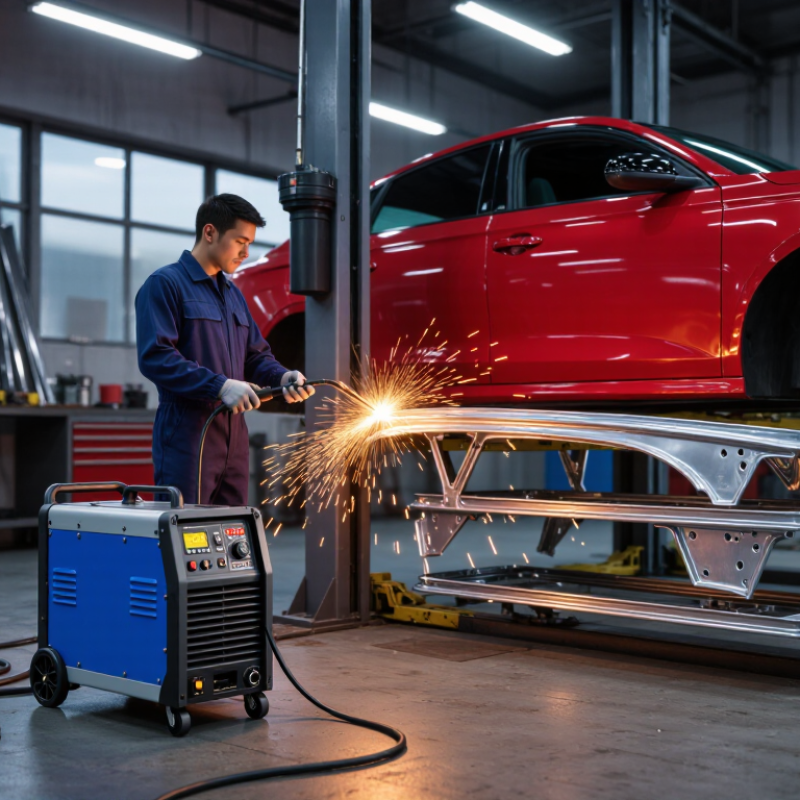
10 Tips for Choosing an Automotive Spot Welder?

Define the Automotive Spot Welder’s Purpose and Required Applications

Before choosing an automotive spot welder, define the work it must perform. A repair shop restoring door panels needs different capacity from a facility joining structural rails. I have seen operators select equipment by price, then struggle with weak welds and limited throat depth. The purpose should be written in practical terms: repair, production, prototype work, or mixed use. Keep it specific. Record the metals, thickness ranges, joint shapes, and weekly workload. These details reveal the machine’s real requirements.

For mild steel body panels, check current control, electrode pressure, and weld-time accuracy. Galvanized or high-strength steel may require tighter settings and stronger clamping force. Do not assume one program fits every panel. It rarely does. Measure the narrowest access point before selecting the arm or throat design. A long reach can help, but it may reduce handling comfort and stability. Also examine cooling performance, duty cycle, and electrode replacement access. A welder that overheats during repeated repairs can delay work and hide inconsistent results.

Match the machine to documented repair procedures and the technician’s training level. Reliable results come from controlled trials, visual inspection, and periodic destructive testing on sample coupons. Follow applicable workplace electrical and personal-protection requirements. Keep records of settings and material combinations. This supports repeatability and helps identify drift. I would leave room for uncertainty, too; real panels are rarely perfectly clean or flat. A small test weld may prevent a costly mistake. Ask whether the chosen machine handles tomorrow’s applications, not only today’s workload.

10 Tips for Choosing an Automotive Spot Welder: Define the Purpose and Required Applications

Welding current is a primary selection factor. Typical automotive applications require different current capacities depending on the metal type and sheet construction. Use these ranges as initial engineering guidance, then validate them with the component supplier and weld-quality testing.

Selection insight: Mild and galvanized steels generally use lower current levels, while advanced high-strength steel and aluminum require higher-capacity equipment. When defining the welder’s purpose, also check material thickness, electrode force, duty cycle, cooling method, controller accuracy, and access to the weld location.

Check Welding Power, Current Range, and Duty Cycle

10 Tips for Choosing an Automotive Spot Welder?

Check Welding Power, Current Range, and Duty Cycle

When evaluating an automotive spot welder, begin with usable welding power, not the highest number printed on a datasheet. Thin galvanized steel may need modest energy, while layered structural panels require stronger, stable output. A machine should deliver consistent current through clean, well-aligned electrodes. Ask whether its transformer or inverter maintains performance during repeated welds. In a busy repair bay, voltage drops and long cables can quietly weaken results. Measure the real setup.

Current range matters because vehicle panels rarely share one thickness. A narrow range can cause burn-through on thin sheet or weak nuggets on stacked metal. Look for fine adjustment, clear readings, and control over weld time. For example, a 0.8 mm panel and two overlapped layers need different settings. Test coupons first. Inspect the nugget after destructive testing, even when the surface looks perfect. It is slower, but revealing.

Duty cycle describes how long the welder can work before cooling. A high peak current is less useful if thermal protection interrupts every few welds. Compare duty-cycle ratings at the current you actually expect to use, not only at a low test setting. Watch electrode arms, cables, and cooling airflow during a long repair session. Practical rhythm matters more than impressive specifications. My first setting is rarely ideal. Record adjustments, allow cooling time, and follow the equipment manual and workshop safety procedures.

10 Tips for Choosing an Automotive Spot Welder? — Check Welding Power, Current Range, and Duty Cycle

Tip Selection Dimension What to Check Typical Automotive Reference Why It Matters
1 Welding Power Confirm the transformer or inverter power rating and whether the output is sufficient for the required sheet-metal thickness. 10–25 kVA is common for many repair and light fabrication applications; higher power may be needed for thicker or high-strength steel. Adequate power helps the machine form consistent weld nuggets without excessive voltage drop or long weld times.
2 Welding Current Range Check the usable secondary current range, adjustment steps, and whether the machine can maintain current under load. 4,000–12,000 A covers many automotive body-repair tasks; specialized equipment can provide more. Different materials and thickness combinations require different current levels. A wider, stable range improves process flexibility.
3 Duty Cycle Review the rated duty cycle, test conditions, cooling method, and recommended operating time at the intended current. 10–30% may be suitable for intermittent body repair; production work generally requires a higher effective duty cycle. A suitable duty cycle reduces thermal shutdowns and keeps weld quality stable during repeated operations.
4 Material and Thickness Capacity Match the rated capacity to galvanized steel, mild steel, high-strength steel, and the maximum combined thickness to be welded. Many automotive repair welders handle approximately 0.6–3.0 mm combined steel thickness, depending on material grade and electrode configuration. High-strength and coated steels may require greater current, accurate timing, and suitable electrode force compared with mild steel.
5 Electrode Force Look for adjustable, repeatable electrode pressure and verify that the arms and tips can reach the repair area. 2–8 kN is a practical reference range for many automotive sheet-metal applications, subject to joint design and material. Correct force controls contact resistance, limits expulsion, and helps produce a properly sized weld nugget.
6 Weld-Time Control Choose a controller with adjustable squeeze, weld, hold, and cool times, preferably with repeatable digital settings. A typical weld pulse may be approximately 5–20 cycles on a 50/60 Hz power system, but the correct value depends on material and thickness. Precise timing helps balance heat input, reduce burn-through, and achieve consistent results across repeated welds.
7 Cooling System Check whether the unit uses air or water cooling, and verify cooling flow, hose connections, and maintenance requirements. Air cooling can suit low-volume work; water-cooled transformers, arms, and electrodes are generally preferred for frequent or high-current operation. Effective cooling protects the transformer, cables, and electrode holders while supporting a higher sustained work rate.
8 Electrode Access and Arm Design Evaluate throat depth, arm length, gun weight, swivel range, tip shape, and access to curved or confined body panels. A portable gun with a flexible cable and interchangeable tips is useful for vehicle panels; fixed-arm designs can offer better repeatability. Good access prevents awkward positioning and helps maintain consistent alignment and pressure at the weld location.
9 Electrical and Facility Requirements Verify input voltage, phase, maximum input current, circuit protection, cable size, grounding, and available shop capacity. Small and medium units commonly use single- or three-phase industrial power; the required supply must be confirmed from the machine specification. Correct facility planning prevents nuisance tripping, overheating, poor output performance, and unsafe installation conditions.
10 Safety, Monitoring, and Serviceability Look for thermal protection, current or energy monitoring, fault indicators, emergency-stop provisions, replaceable tips, and accessible service points. Useful features include over-temperature protection, weld counters, programmable settings, water-flow monitoring, and documented preventive-maintenance intervals. Monitoring and service access improve operator safety, traceability, uptime, and long-term welding consistency.

Note: The ranges shown are general industry references rather than universal limits. Always confirm the machine’s tested capacity, electrode configuration, material grade, and local electrical requirements before purchase.

Evaluate Electrode Design, Arm Reach, and Material Compatibility

10 Tips for Choosing an Automotive Spot Welder

Electrode design often determines weld consistency more than advertised power. Choose caps that match the panel thickness, weld diameter, and access angle. Copper alloys transfer current efficiently, while replaceable caps reduce maintenance costs. Flat tips suit overlapping sheets, but angled or offset tips may reach narrow door frames. Check the electrode dressing method before purchase. It should be practical on a busy workshop floor.

Arm reach matters when panels are large or deeply recessed. Measure the distance from the machine body to the intended weld points. A short arm may force awkward positioning and uneven pressure. A longer arm improves access, but it can flex under load. That detail is easy to miss. I once tested a welder that reached every point, yet produced inconsistent welds near the arm’s limit. The design looked capable, but the real-world stiffness was disappointing.

Material compatibility requires careful attention. Standard low-carbon steel, galvanized steel, and advanced high-strength steel can need different current, force, and weld-time settings. Aluminum usually demands specialized equipment because it conducts heat quickly and requires higher current. Review the welder’s tested material range, not only its maximum output. Inspect cable size, cooling performance, and electrode pressure ratings as well. Trial welds on matching scrap are valuable. Record nugget size, surface marks, and pull-test results. One setting rarely suits every panel. Supplier documentation helps, but hands-on verification remains essential.

Compare Safety Features, Controls, Portability, and Maintenance

Choosing an automotive spot welder requires more than comparing welding power. Safety features, controls, portability, and maintenance affect daily results. Look for thermal overload protection, insulated handles, secure grounding, and a clear emergency stop. A guarded trigger helps prevent accidental activation. Proper ventilation still matters, even with a well-designed machine.

Tip 1: Test the controls before purchase.

Current, weld time, and electrode pressure should adjust smoothly. Digital displays can improve repeatability, but only when readings are easy to see through welding gloves. I once underestimated awkward controls. That mistake slowed every repair.

Portability matters in crowded workshops. Check the unit’s weight, cable length, cooling design, and wheel stability. A compact welder is useful near a vehicle, but a short cable can create unsafe positioning. Choose a model that reaches the work area without stretching or dragging across walkways.

Tip 2: Inspect maintenance access.

Replaceable electrodes, accessible cooling vents, and simple cable connections reduce downtime. Clean metal dust regularly, and inspect insulation before each shift. Keep a maintenance log with weld counts and visible wear. It may feel excessive, but small cracks can become expensive failures. Always test settings on scrap panels before touching a finished vehicle.

Assess Cost, Warranty, Certifications, and Supplier Support

10 Tips for Choosing an Automotive Spot Welder

Tip 1: Compare the total cost, not only the purchase price. Include electrodes, cooling parts, installation, training, and expected maintenance. Tip 2: Check whether the welder suits your materials and sheet thickness. A cheap unit may struggle with high-strength steel. Tip 3: Ask for measured energy consumption. Your workshop’s daily workload can change the real cost quickly. Tip 4: Review the warranty carefully. Confirm coverage for transformers, cables, controls, and cooling systems. Short coverage may indicate expensive risks.

Tip 5: Verify that certifications apply to the exact model, not just the manufacturer. Look for recognized electrical safety and quality documentation. Tip 6: Request inspection records and test procedures. Clear documents are more useful than impressive claims. Tip 7: Ask how quickly replacement parts can arrive. A two-day delay can stop an entire repair bay. Tip 8: Test supplier support before buying. Send technical questions and judge the accuracy of the reply. Good support should explain settings, not simply send a brochure.

Tip 9: Request operator training, preferably with practical demonstrations on similar panels. I have found that hands-on guidance prevents poor welds and wasted sheets. Tip 10: Clarify software updates, troubleshooting, and remote assistance. These details are easy to overlook. Also, ask for references from workshops with comparable workloads. I once focused too heavily on output power and underestimated service access. That mistake made routine maintenance slower than expected. A small trial can reveal more than a polished sales presentation.

Contact us

Please fill out the enquiry form, and our dedicated team will promptly attend to your request